Cosmetic Packaging Inspection: What We Check Before Loading
Cosmetic packaging inspection follows the same route every time. Two hours on the floor. Weeks of email saved.
Before anything is packed
Three documents come first.
A golden sample, signed by both sides. Colour code and date on the label.
A specification sheet. Capacity and neck finish (24/410, 28/410). Height, body diameter, unit weight, resin. Pantone colour, decoration method, pump model, units per carton.
A defect table. Critical, major, minor. An acceptance decision beside each one.
Two signatures, one date. That is all a good reference needs.
Skip the third document and one speck becomes a negotiation. Classify it and the lot moves on.
We photograph the signed sample the day it is signed. Physical references disappear in warehouses. A dated photo has settled arguments for us more than once.
On the floor, part by part
Colour goes into a light booth. Warm workshop lamps make pale green and pale grey look like the same colour.
Then surfaces. The consumer-visible panel first, the thread interior after. Same limits on both and the scrap rate stops being workable. Black spots, oil marks, sink marks, flow lines, flash, scratches. Counted by class.
Dimensions against the drawing. Height, neck diameter, body diameter, wall thickness. Capacity by filling to the nominal line. A 100 ml bottle that holds 96 ml is a problem. It shows up on the customer's filling line, not ours.
Assembly by hand. Cap on, pump pressed, filled unit inverted, seam watched. Fifteen seconds per unit.
Pull samples from sealed cartons. Pieces set aside in advance tell you nothing about the shipment.
Function, then decoration
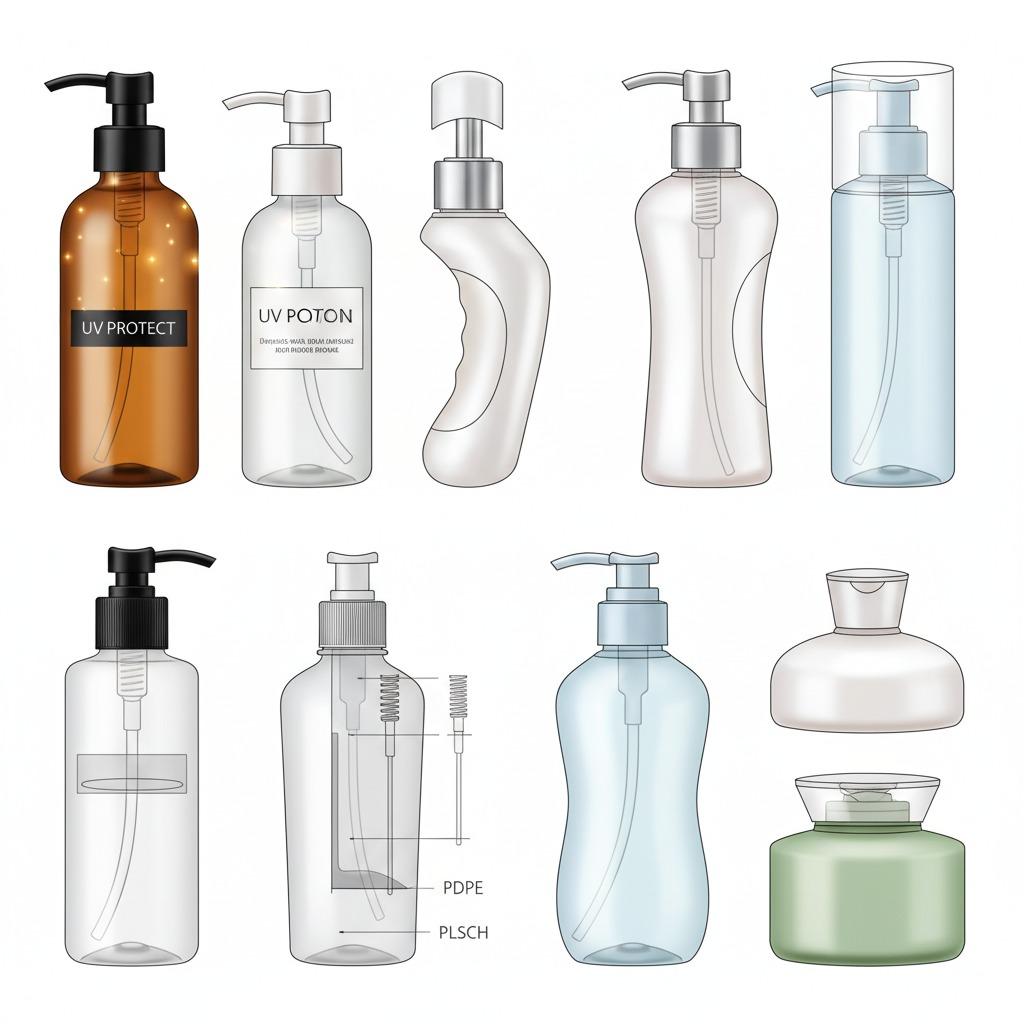
Dose consistency is where most cosmetic packaging inspection findings come from. 10 to 20 units, the agreed number of presses, output per stroke recorded. Air locking, a pause mid-stroke, a slow return. Any one of those stops a filling line.
Spray bottles. Dark board, upright, inverted, held down without a break. Even atomisation, no stream where a mist was promised, no drip at the nozzle. A short dip tube shows up inverted. A tired gasket shows up on the long hold.
Foam pumps. Consistent foam from press to press. Air tightness is the weak point.
Sealing. Inverted cold, then inverted warm. Water bath or vacuum check where the specification calls for it. Torque in newton centimetres, measured with a gauge. Not by wrist.
Compatibility. Pack against the real formula, or a simulant. Essential oils, acids, high-alcohol formulas. Skipped in peak season, discovered six weeks after the goods shipped.
Decoration. Cross-hatch tape pull per ASTM D3359. A 75% ethanol rub. Edges on hot-stamped parts, pinholes on silk-screened parts. Flat proofs lie about curved bodies. First-off pieces get photographed and confirmed before the batch runs.
Shipping, sampling, failures
Sampling follows ISO 2859-1. General inspection level II. AQL 2.5 for major defects, 4.0 for minor. Put it in the purchase order next to the defect table.
Go 100% in three cases. A first mass-production run. The first-off piece from a new mould. Complex decoration.
Cartons. Stacked weight lands on the pump actuator. Reverse assembly, protective caps and internal dividers fix that. Parts rub together, and matte or hot-stamped finishes take scratches that cannot be polished out. Unit bags fix that. Check board grade against the real stacking height. Protect pallet corners. Keep cartons off the container wall. Photograph the stacking configuration before dispatch.
A cosmetic packaging inspection ends one of three ways when a lot fails. Rework, then re-inspection. Sample size no smaller than the first. Concession, for defects that touch neither function nor the visible panel. Written approval first. Then an agreed position on price or restricted use. Remake, when the schedule matters more than assigning blame.
Retention samples stay until the warranty ends. Indexed by lot number and inspection report.
Send the specification and the sample. We come back with an article number, the mould situation and a quotation. Contact us for samples. Product families: spray bottles, lotion and pump bottles, cream jars, tubes.